PU Adhesive for Marble Edge Bonding: A Practical Guide to Professional Stone Fabrication
Marble edge bonding is a detail-oriented fabrication task where accurate preparation, dry fitting, controlled adhesive application and alignment all work together. This guide explains the process step by step and shows where a compatible two-component PU adhesive can fit into the workflow.
Explore DUSH Arena Duo View on Flipkart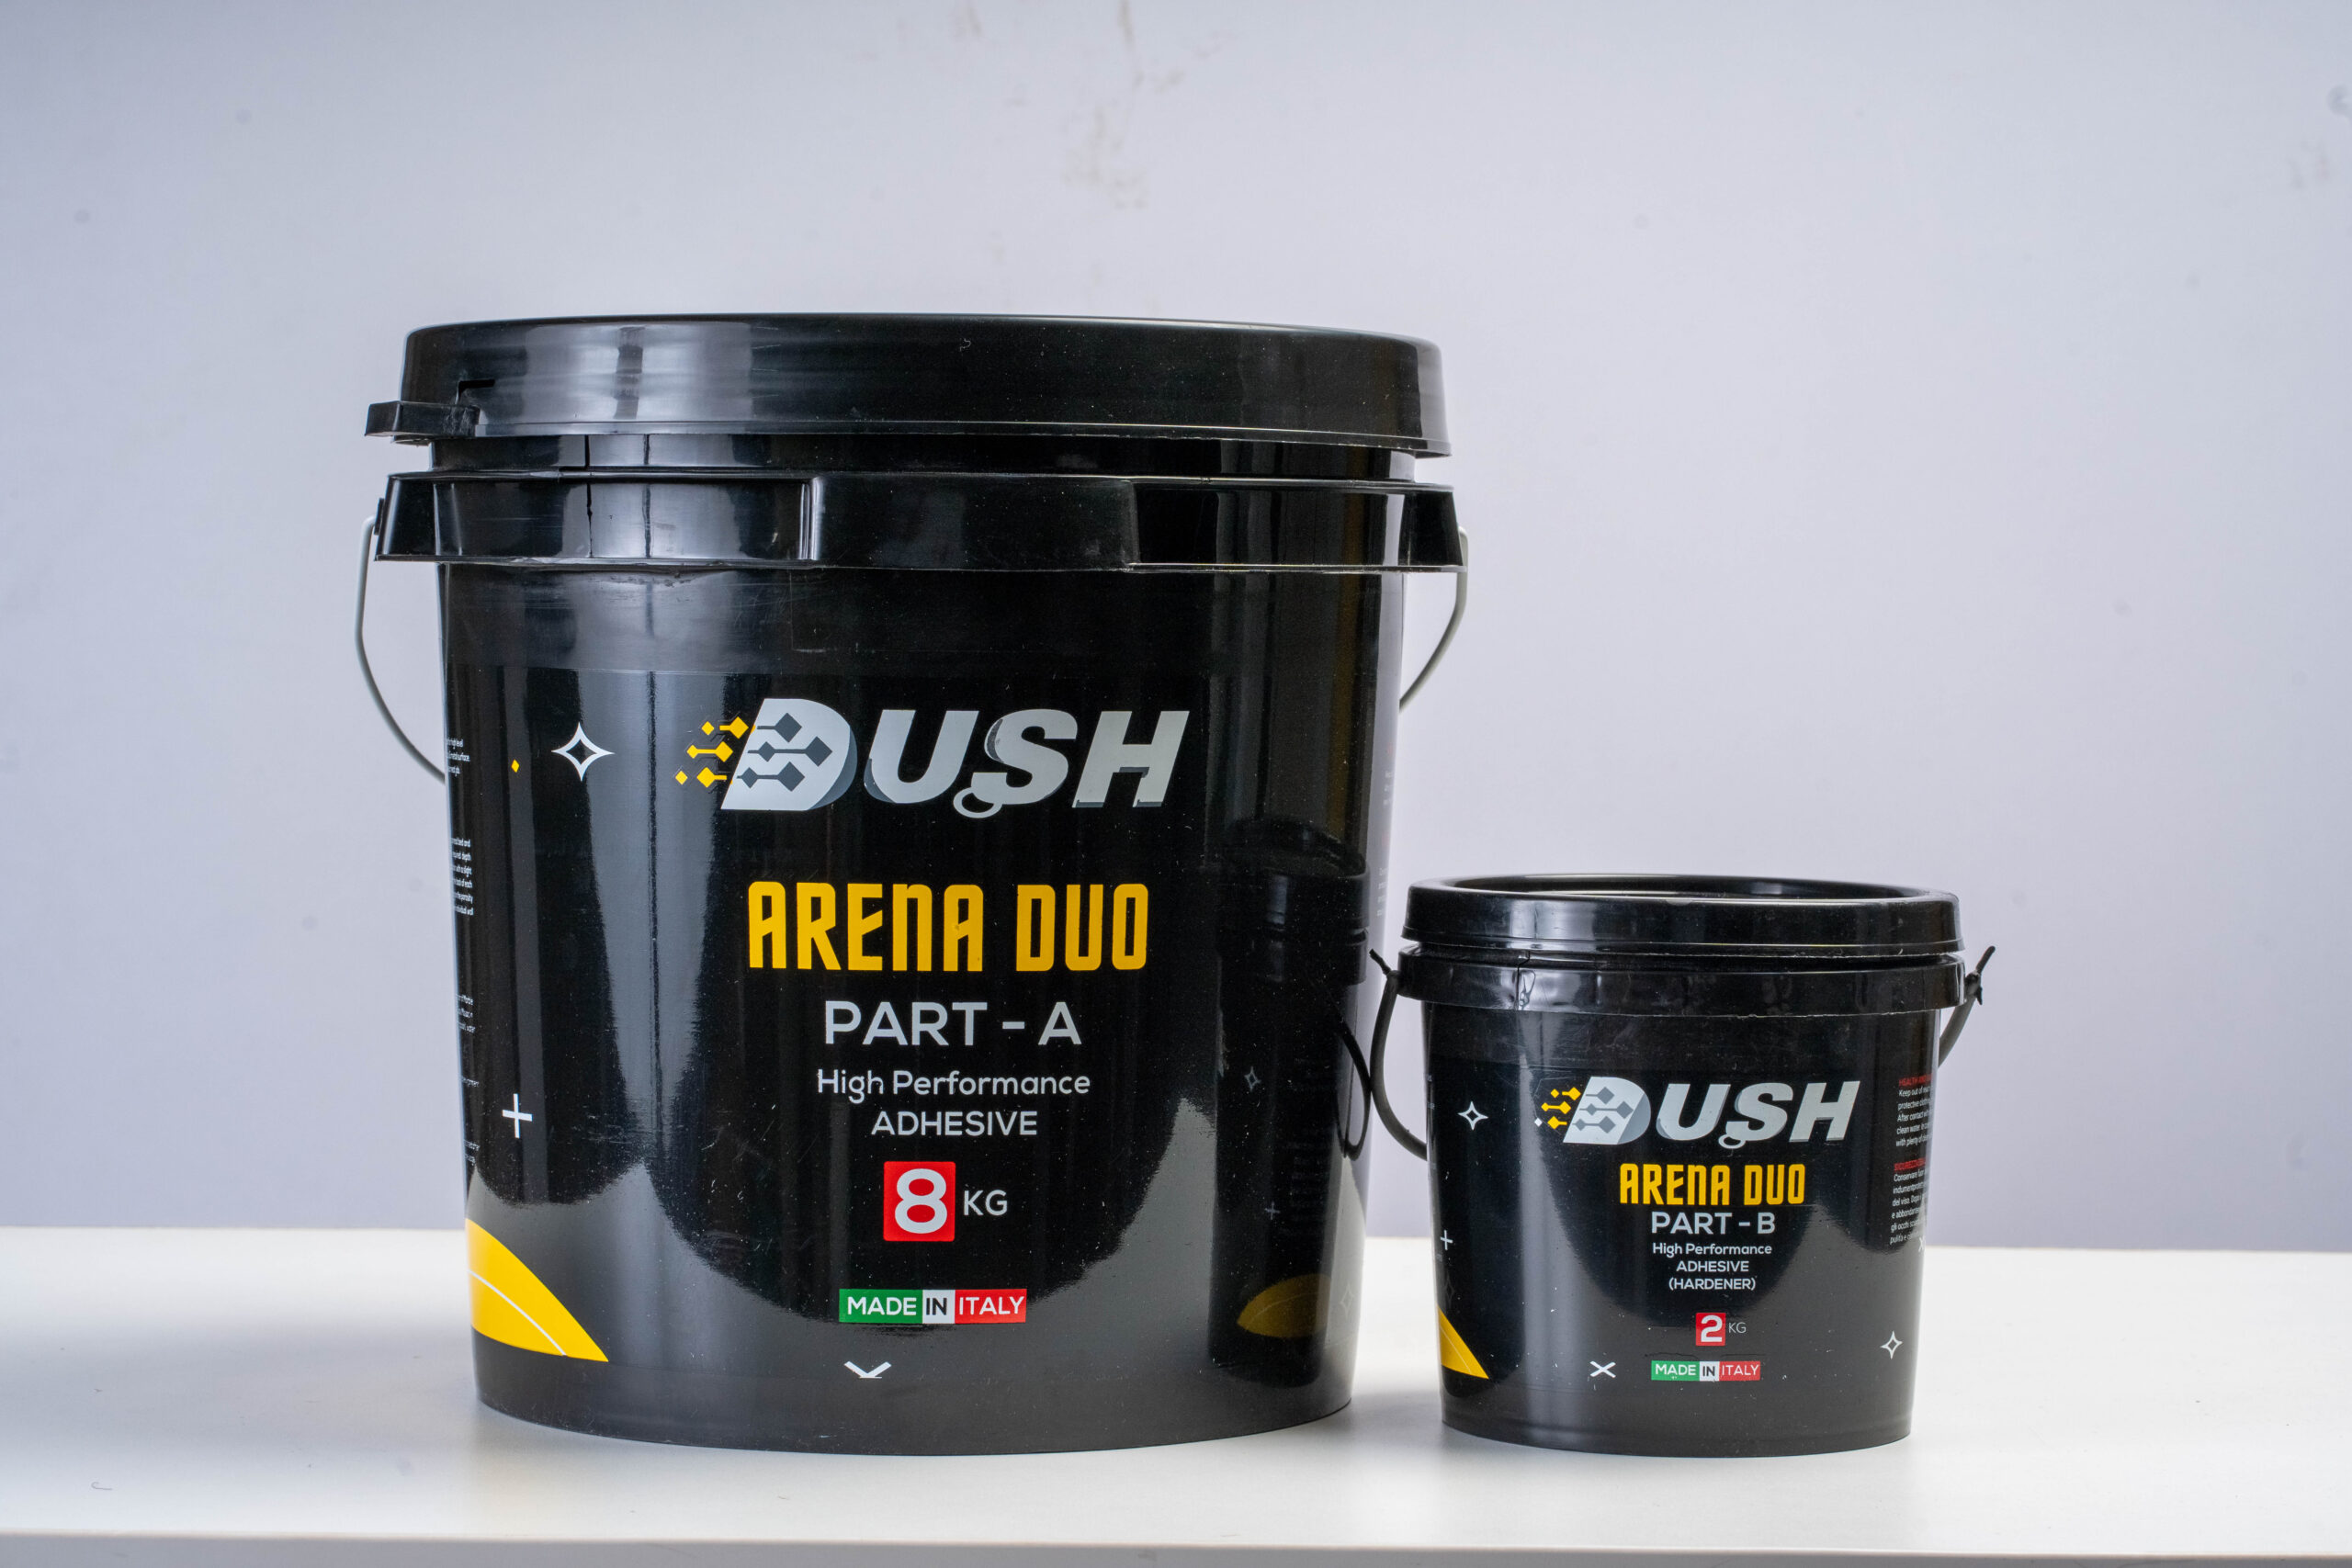
Marble edge bonding is a fabrication operation, not simply an adhesive application. The quality of an edge assembly depends on the accuracy of the fabricated pieces, the condition of the bonding surfaces, the fit of the joint and the way the parts are held after adhesive is applied.
When a compatible PU adhesive is selected for the intended application, the best results come from treating bonding as part of the fabrication sequence. The edge should be planned, prepared and dry fitted before the adhesive is mixed.
1. What Is Marble Edge Bonding?
Marble edge bonding is the process of joining fabricated marble components along an edge or prepared interface to create a larger or more complete assembly. It can be relevant when separate pieces need to work together as one fabricated component.
The visible result may depend on several factors at once: edge accuracy, joint alignment, adhesive application, component positioning and subsequent finishing. This is why edge bonding should be approached as a controlled workshop process.
2. Why Edge Preparation Matters
The adhesive is only one part of the joint. Before bonding begins, the fabricated edges need to be inspected for the intended geometry and fit.
Accurate Geometry
The two components should be fabricated to the intended dimensions and edge profile before adhesive is introduced.
Clean Interface
The bonding area should be prepared according to the adhesive manufacturer's instructions and free from conditions that may interfere with the bond.
Controlled Alignment
The parts should have a planned positioning method so the intended edge relationship can be maintained while the bond develops.
Dry-Fit Confirmation
A dry fit allows the fabricator to identify fit or alignment issues before adhesive working time begins.
3. Where Marble Edge Bonding Can Be Used
Edge bonding can appear in different fabrication assemblies. The exact method depends on the project geometry and the materials being joined.
| Fabrication situation | What to evaluate before bonding |
|---|---|
| Marble-to-marble edge assembly | Edge geometry, surface condition, dry fit, alignment and the intended joint appearance. |
| Natural-stone edge assembly | Actual stone type, surface characteristics and compatibility with the selected adhesive. |
| Stone-to-glass interface | Confirm that the intended materials and application are documented as compatible and prepare each interface appropriately. |
| Stone-to-metal or aluminium assembly | Consider the different substrate characteristics and verify compatibility before production bonding. |
| Composite-related assembly | Identify the exact composite material instead of assuming all composite surfaces behave identically. |
4. Step-by-Step Marble Edge Bonding Workflow
A consistent sequence helps keep adhesive work under control. The following workflow is a practical framework and should be adapted to the current adhesive instructions and the actual fabrication assembly.
Inspect the Fabricated Parts
Check the marble components for dimensions, edge profile, visible defects and the condition of the intended bonding areas.
Dry Fit the Edges
Bring the pieces together without adhesive. Check how the edges meet, whether the alignment is correct and whether the planned joint can be assembled smoothly.
Plan the Holding Method
Decide how the pieces will remain in position after adhesive application. The method depends on the component geometry and workshop setup.
Prepare the Surfaces
Prepare the bonding interfaces according to the product instructions. Do not assume the same preparation method applies to every material.
Prepare the Adhesive
Measure and combine the adhesive components using the specified ratio. DUSH Arena Duo has a published 2:1 mixing ratio.
Apply to the Bonding Interface
Apply the adhesive to the intended bonding area using a controlled process appropriate to the product and joint.
Join and Align
Bring the marble components together and check the edge relationship immediately. Make required positioning adjustments while the adhesive remains workable.
Hold and Inspect
Maintain the assembly in its intended position during the relevant curing period, then inspect the finished joint before the next fabrication stage.
5. Why Dry Fitting Comes Before Adhesive
Dry fitting is one of the most useful checks in an edge-bonding workflow because it separates fabrication problems from adhesive problems.
Without adhesive, the fabricator can check:
- Whether the edges meet as intended.
- Whether the components are correctly oriented.
- Whether the joint position is practical for application.
- Whether the components can be positioned without excessive movement.
- Whether clamps, supports or temporary fixtures are required.
If the dry fit is not satisfactory, mixing adhesive does not solve the underlying fabrication issue. Correct the assembly first.
6. Surface Preparation Before Marble Edge Bonding
Surface preparation should be based on the adhesive manufacturer's current instructions and the actual materials being joined.
Inspect the bonding zone
Look specifically at the surfaces that will receive the adhesive. Finished faces should be protected from unnecessary contamination, while the bonding interface should be prepared as required.
Keep the sequence controlled
Prepare the bonding surfaces close enough to the bonding operation that they remain in the required condition. Avoid introducing contaminants after preparation.
Do not use adhesive to compensate for poor fit
A bonding product is not a replacement for accurate fabrication. If an edge is incorrectly cut or the components do not align as designed, the joint should be addressed before bonding.
7. Mixing a Two-Component PU Adhesive
A two-component adhesive relies on the components being combined in the specified proportion. The mixing stage should therefore be treated as a controlled part of the fabrication process.
For DUSH Arena Duo, the published mixing ratio is 2:1.
The published open time is approximately 30–45 minutes. For a workshop, that means the fabricator should have the components ready, the edge dry fitted and the positioning method planned before the adhesive is prepared.
Workshop planning around open time
- Complete the dry fit before mixing.
- Keep all required tools and supports ready.
- Prepare the bonding surfaces.
- Confirm the assembly sequence.
- Mix the adhesive according to the published ratio and product instructions.
- Move efficiently through application and positioning.
Open time should be treated as a planning reference rather than a guarantee that every assembly can be completed within the same period under all conditions. Environmental conditions, joint size and the actual workflow can affect how a job should be managed.
8. Applying PU Adhesive to a Marble Edge
Once the surfaces and components are ready, adhesive application should be controlled and consistent.
A practical sequence is:
- Confirm the dry-fit position one final time.
- Prepare the adhesive using the specified component ratio.
- Mix according to the manufacturer's instructions.
- Apply the adhesive to the intended bonding interface.
- Bring the two fabricated components together.
- Check the edge alignment immediately.
- Secure or support the assembly as required.
- Allow the bond to develop according to the product instructions.
The goal is not simply to place adhesive between two pieces. It is to create a controlled assembly in which the adhesive, joint geometry and component positioning work together.
9. Alignment Is a Critical Part of Edge Bonding
For marble fabrication, alignment is particularly important because the edge can remain visually significant after the assembly is finished.
Before adhesive is mixed, decide:
- Where the reference edge will be.
- How the components will be brought together.
- How alignment will be checked.
- How the pieces will be supported after positioning.
- How unnecessary movement will be minimized while the bond develops.
10. Managing Excess Adhesive During Fabrication
Controlled application helps reduce unnecessary adhesive around finished surfaces. Before beginning, the fabricator should understand the product's application and cleanup requirements.
Visible marble faces and polished areas should be protected where appropriate. Any cleanup procedure should follow the manufacturer's recommendations and should not introduce damage to the finished stone surface.
It is also useful to plan the direction from which the adhesive will be applied and how the components will be brought together. A planned sequence is easier to control than improvising after adhesive has already been mixed.
11. Holding the Marble Edge During the Bonding Period
After positioning, the components should remain controlled during the relevant curing period. The holding method will depend on the shape, size and weight of the fabricated pieces.
Possible workshop approaches can include suitable temporary supports, fixtures or clamps where appropriate. The chosen method should hold the components in their intended position without creating unnecessary stress or damaging the finished stone.
The key point is simple: alignment does not end when the pieces touch. It needs to be maintained for the relevant stage of the bonding process.
12. Marble Edge Bonding Quality Checklist
| Checkpoint | What to verify |
|---|---|
| Fabrication accuracy | Are the components cut and profiled according to the intended design? |
| Material compatibility | Is the selected adhesive documented for the actual materials and application? |
| Edge condition | Are the bonding interfaces prepared as required? |
| Dry fit | Do the components meet and align correctly without adhesive? |
| Holding method | Is there a practical way to keep the parts aligned after bonding? |
| Mix ratio | Have the adhesive components been combined in the specified proportion? |
| Working time | Can the planned assembly be completed within the applicable working period? |
| Final alignment | Has the edge position been checked immediately after joining? |
| Post-bond inspection | Has the completed assembly been inspected before moving to finishing or installation? |
13. Common Marble Edge Bonding Mistakes
1. Skipping the dry fit
Starting with adhesive before checking the joint can turn a simple fabrication correction into a time-sensitive bonding problem.
2. Mixing the adhesive too early
If the parts, tools and holding method are not ready, useful working time can be consumed before the actual assembly begins.
3. Assuming all stone surfaces are identical
Different natural stones and finishes can have different characteristics. The actual material and application should be checked for compatibility.
4. Focusing only on adhesive coverage
A good edge assembly also depends on fabrication accuracy, joint fit and positioning. Adhesive application cannot replace those steps.
5. Moving the assembly unnecessarily
Once the components have been positioned, unnecessary movement can interfere with controlled bonding. The assembly should be managed according to the product instructions.
6. Using a generic preparation method
Stone, glass, metal, aluminium and composite interfaces can differ. Preparation should be based on the actual substrate and product documentation.
14. DUSH Arena Duo for Marble and Stone Bonding
DUSH Arena Duo
DUSH Arena Duo is a two-component PU adhesive. Its published applications include natural stone and marble with compatible glass, metal, aluminium and composite surfaces.
| Product type | Two-component PU adhesive |
|---|---|
| Published mixing ratio | 2:1 |
| Published open time | Approximately 30–45 minutes |
| Documented application materials | Natural stone / marble with compatible glass, metal, aluminium and composite surfaces |
15. DUSH Arena Duo Product Video
16. What About Stone-to-Glass, Metal, Aluminium or Composite Edges?
Edge bonding is not limited to stone-to-stone assemblies. DUSH Arena Duo documentation discusses applications involving natural stone or marble with compatible glass, metal, aluminium and composite surfaces.
When two different materials are joined, the fabricator should treat the interfaces as a specific engineering and preparation task. The surfaces may have different characteristics, and the intended application should be checked against the current product documentation.
Do not interpret a general material category as automatic approval for every grade, finish, coating or assembly. The exact materials should be verified before production use.
17. Building a Repeatable Edge-Bonding Process
For workshops performing repeated fabrication work, consistency can be improved by turning the bonding sequence into a standard internal process.
- Step 1: Identify the materials and intended assembly.
- Step 2: Fabricate the components to the required geometry.
- Step 3: Dry fit the edges.
- Step 4: Prepare the bonding interfaces.
- Step 5: Prepare the holding and alignment method.
- Step 6: Measure and mix the adhesive according to the product instructions.
- Step 7: Apply, join and align the components.
- Step 8: Maintain the assembly during the relevant curing stage.
- Step 9: Inspect before finishing, installation or release.
This process helps separate the fabrication stage from the bonding stage while keeping them connected through planned checkpoints.
18. Final Takeaway
Successful marble edge bonding starts before the adhesive is mixed. Accurate fabrication, proper dry fitting, surface preparation, a planned holding method and controlled alignment all contribute to a more organized bonding workflow.
For compatible applications, DUSH Arena Duo offers a two-component PU adhesive with a published 2:1 mixing ratio and approximately 30–45 minutes of published open time. The actual material compatibility and application should always be confirmed using the latest product documentation before production use.
Looking for a PU Adhesive for Marble Fabrication?
Explore DUSH Arena Duo and review its documented applications before selecting it for your marble or natural-stone bonding assembly.
Explore DUSH Arena Duo Visit DUSH ProductsFrequently Asked Questions
What is PU adhesive used for in marble edge bonding?
PU adhesive can be used for compatible marble and stone bonding applications where fabricated components need to be joined. The exact suitability depends on the materials, joint design, surface preparation and product instructions.
Why is dry fitting important before marble edge bonding?
Dry fitting allows the fabricator to check the edge geometry, alignment, joint position and holding method before adhesive is mixed and applied.
What is the mixing ratio of DUSH Arena Duo?
The published mixing ratio for DUSH Arena Duo is 2:1.
What is the published open time of DUSH Arena Duo?
The published open time for DUSH Arena Duo is approximately 30–45 minutes.
Can DUSH Arena Duo be used with materials other than marble?
DUSH Arena Duo documentation discusses applications involving natural stone or marble with compatible glass, metal, aluminium and composite surfaces. Exact compatibility should be checked for the intended assembly.
Product note: Specifications and application guidance can change. Always refer to the latest DUSH product documentation and follow the applicable instructions for the specific project.